Huahui is one of the China leading manufacturers of industrial steel valves, recognized as a standard-bearer in quality and innovation. The company was founded in 2006, and continues to leverage advanced engineering capabilities and innovation to create hard-working valves that meet critical industrial needs in the areas of power generation, chemical and petrochemical, oil and gas, pulp and paper, mining, cryogenic, and ship-building industries.Huahui's product lines are grouped into the broad categories of: steam traps; strainers; specialty valves and exhaust valves. Within these product groups, Huahui offers one of the most comprehensive product offerings available from any valve manufacturer, in sizes varying from 1/2” to 60”, with pressure ratings from vacuum to over 10,000 psi, temperature ratings of up to 1,500°F, and availability of many material and design options. All of Huahui's valves are designed and manufactured with quality as a priority, and incorporate many unique design features for environmentally friendly performance, simple maintenance, and reliable service.Huahui valves have an extremely broad installation base and are approved by major companies. In addition, Huahui has been an active and trusted name in the power industry since its inception, and has supplied valves to the vast majority of power stations in the china. We are currently involved in the global renaissance of power, focusing our design, applications, and manufacturing resources on a market that projects a growing number of units to be built.We owe much of our success to the capability, experience, and dedication of our employees who have made quality and innovation the cornerstone of Huahui since its inception. We concentrate on one business-designing, manufacturing and marketing advanced technology steel valves in a broad range of types and sizes. That's why we can truly claim: Huahui. Quality is life.
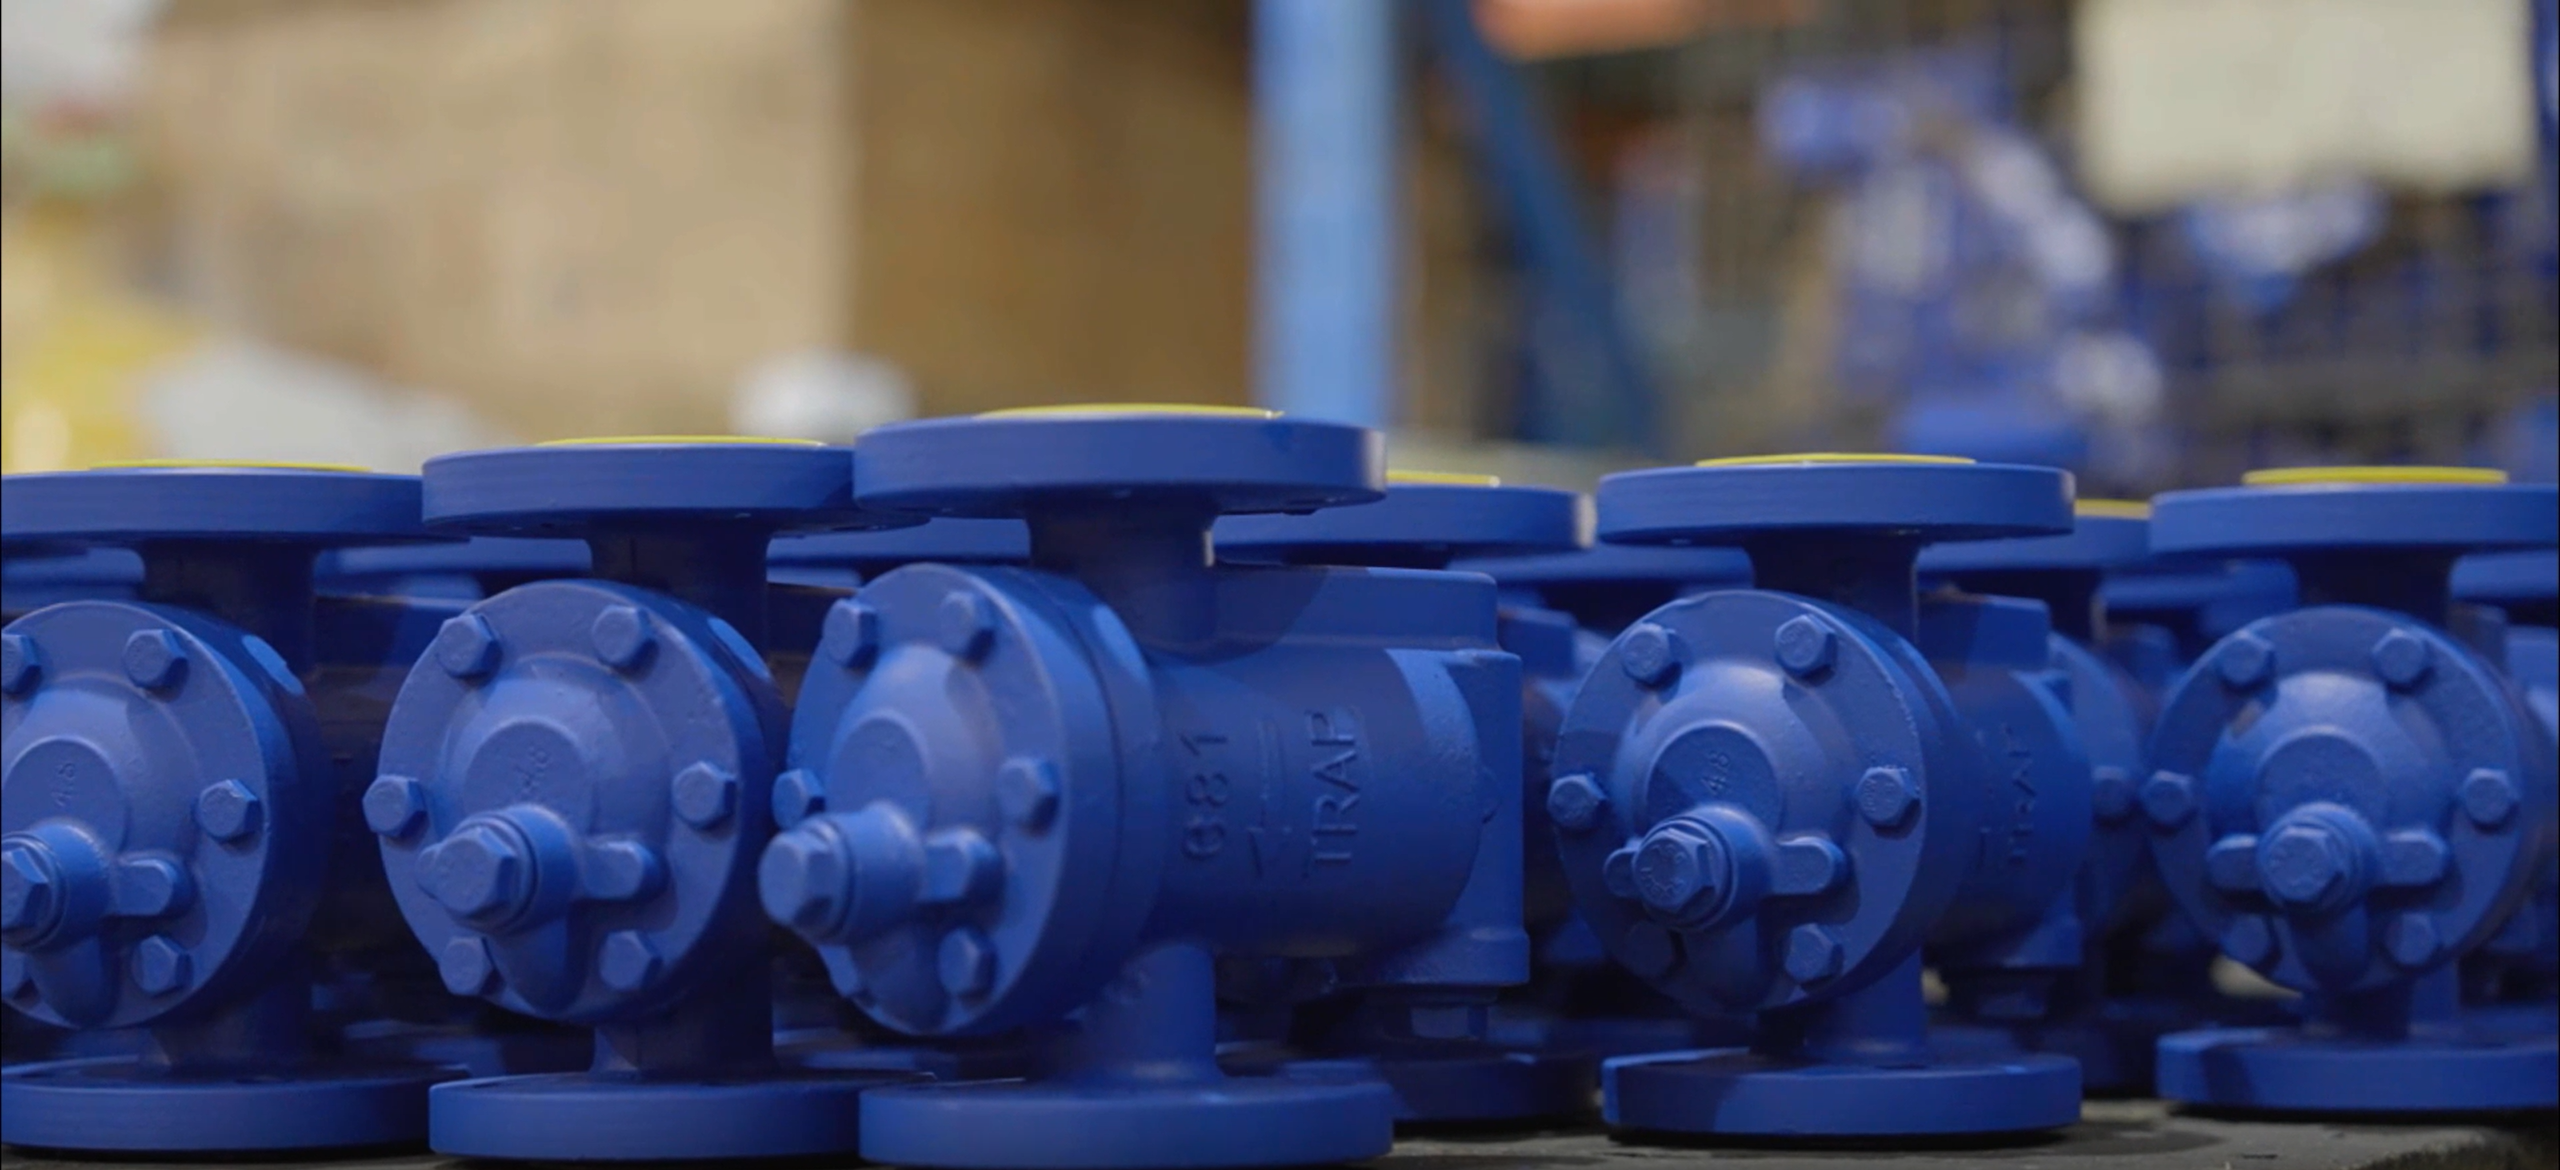


Analysis Of Huahui Inverted Bucket Drain Valve: Reliable Guarantee For Stable Operation
In modern steam systems, steam traps play a crucial role as they directly affect equipment efficiency, system safety, and energy consumption. Inverted bucket drain valve, as a mechanical drain valve with stable performance and strong resistance to water hammer, is widely used in various industrial applications. Zhejiang Huahui Valve Co., Ltd. has formed a mature solution in the field of inverted bucket drain valves with a strong technical foundation and continuous product optimization, meeting the needs of multiple industries and working conditions.

1、 Working principle: Precise control based on density difference
The core principle of the inverted bucket drain valve is to control the opening and closing action by utilizing the difference in density between steam and condensed water. There is an inverted metal float bucket inside the valve body. When condensed water enters, the float bucket sinks and the valve opens for drainage; When steam enters the interior of the floating bucket, the bucket rises and the valve immediately closes, thereby achieving effective drainage and steam retention. Zhejiang Huahui pays attention to optimizing the flow channel structure and sealing performance in product design, ensuring sensitive movement and long-lasting service life.

2、 Product advantages: stability, efficiency, durability
The inverted bucket drain valve produced by Huahui has the following significant advantages:
Strong water hammer resistance: suitable for systems with frequent start stop or fluctuating Pressure to ensure stable system operation;
Low steam loss: action delay design avoids premature closure and reduces steam leakage;
Easy maintenance: The valve body structure is easy to disassemble and maintain, reducing operation and maintenance costs;
Strong adaptability: a variety of Material can be selected to adapt to different temperatures, Pressure and media environments;
Good exhaust function: equipped with automatic exhaust characteristics, effectively reducing equipment start-up time.

3、 Application area: Covering system requirements across multiple industries
Huahui inverted bucket drain valves are widely used in industries such as power, chemical, papermaking, food processing, and heating, especially for controlling condensate discharge in key areas such as heat exchangers, steam pipelines, and drying equipment. Its high stability and convenient maintenance characteristics are particularly prominent in continuous working conditions or situations that require frequent start stop, winning the recognition and trust of many users.
Zhejiang Huahui Valve insists on continuously optimizing the structural design and process control of inverted bucket drain valves, striving to provide customers with stable and efficient steam condensate water management solutions. In the future, Huahui will continue to delve into the field of steam systems with a professional attitude, promote the dual improvement of energy conservation and equipment safety, and create higher value for customers.
 Previous News

Analysis Of Huahui Inverted Bucket Drain Valve: Reliable Guarantee For Stable Operation
In modern steam systems, steam traps play a crucial role as they directly affect equipment efficiency, system safety, and energy consumption. Inverted bucket drain valve, as a mechanical drain valve with stable performance and strong resistance to water hammer, is widely used in various industrial applications. Zhejiang Huahui Valve Co., Ltd. has formed a mature solution in the field of inverted bucket drain valves with a strong technical foundation and continuous product optimization, meeting the needs of multiple industries and working conditions.
1、 Working principle: Precise control based on density difference
The core principle of the inverted bucket drain valve is to control the opening and closing action by utilizing the difference in density between steam and condensed water. There is an inverted metal float bucket inside the valve body. When condensed water enters, the float bucket sinks and the valve opens for drainage; When steam enters the interior of the floating bucket, the bucket rises and the valve immediately closes, thereby achieving effective drainage and steam retention. Zhejiang Huahui pays attention to optimizing the flow channel structure and sealing performance in product design, ensuring sensitive movement and long-lasting service life.
2、 Product advantages: stability, efficiency, durability
The inverted bucket drain valve produced by Huahui has the following significant advantages:
Strong water hammer resistance: suitable for systems with frequent start stop or fluctuating Pressure to ensure stable system operation;
Low steam loss: action delay design avoids premature closure and reduces steam leakage;
Easy maintenance: The valve body structure is easy to disassemble and maintain, reducing operation and maintenance costs;
Strong adaptability: a variety of Material can be selected to adapt to different temperatures, Pressure and media environments;
Good exhaust function: equipped with automatic exhaust characteristics, effectively reducing equipment start-up time.
3、 Application area: Covering system requirements across multiple industries
Huahui inverted bucket drain valves are widely used in industries such as power, chemical, papermaking, food processing, and heating, especially for controlling condensate discharge in key areas such as heat exchangers, steam pipelines, and drying equipment. Its high stability and convenient maintenance characteristics are particularly prominent in continuous working conditions or situations that require frequent start stop, winning the recognition and trust of many users.
Zhejiang Huahui Valve insists on continuously optimizing the structural design and process control of inverted bucket drain valves, striving to provide customers with stable and efficient steam condensate water management solutions. In the future, Huahui will continue to delve into the field of steam systems with a professional attitude, promote the dual improvement of energy conservation and equipment safety, and create higher value for customers.
Previous News
CopyRight©2018 Valve Data Center All rights reserved
customer service hotline:400-633-5118/86-0577-86857700
Valve Data Center - Chinese Valve Service Media, Empowering Global Industrial Safety.

客服

微信公众号

关注抖音号

苹果App

华为App


